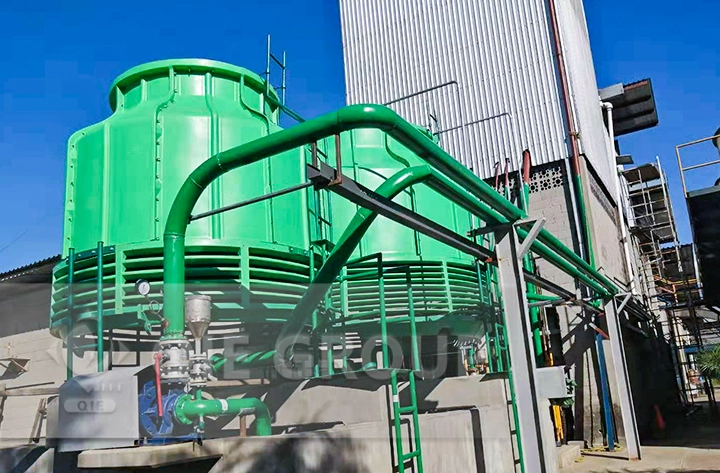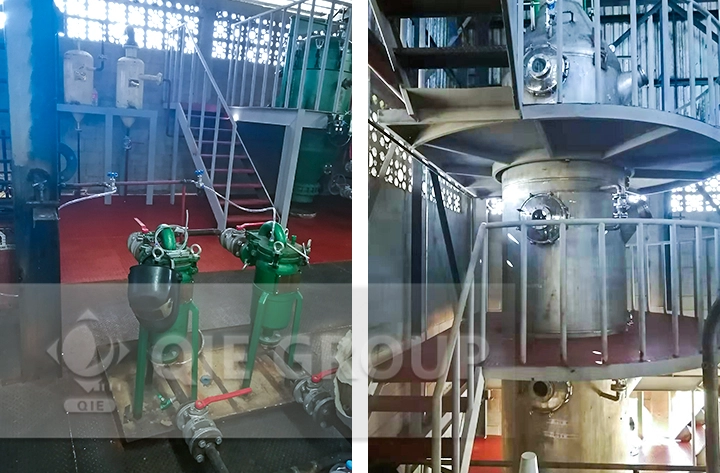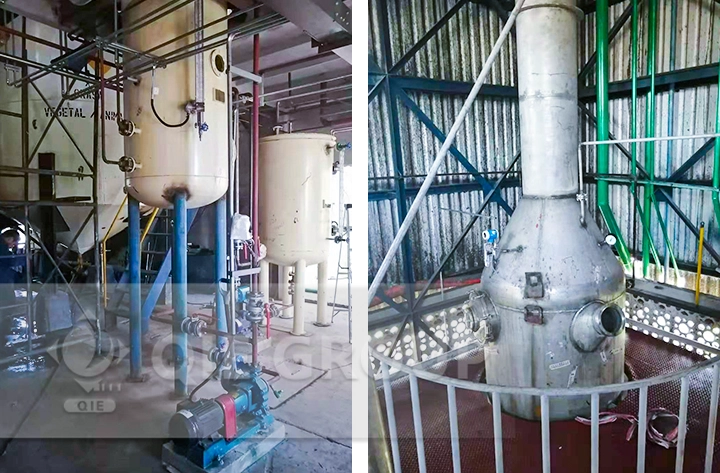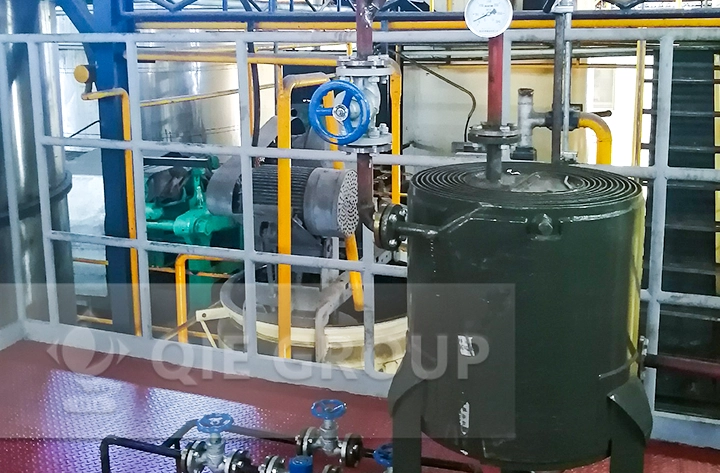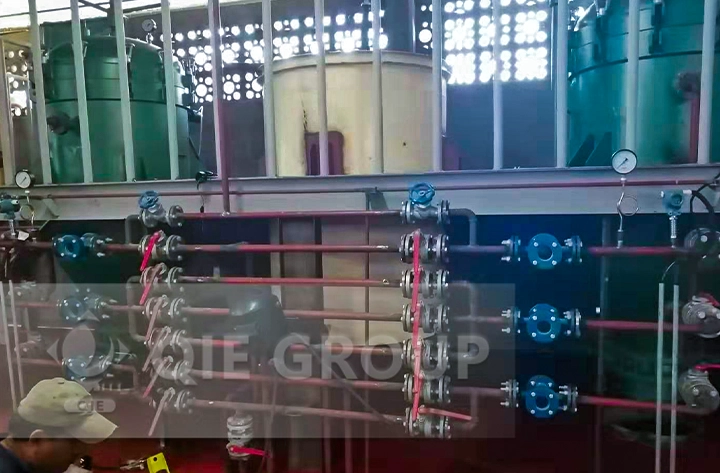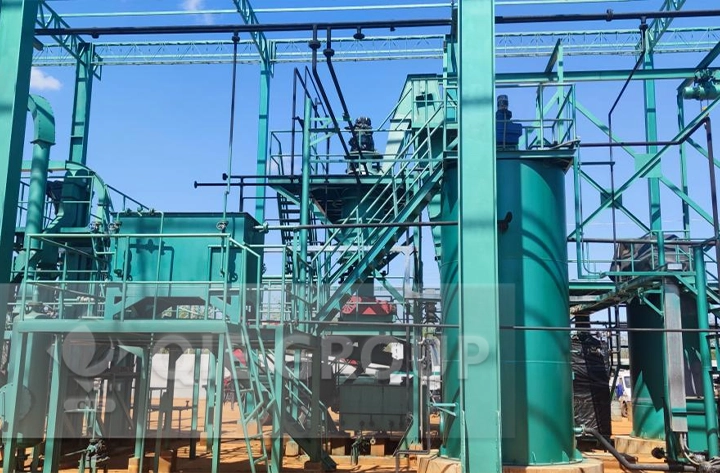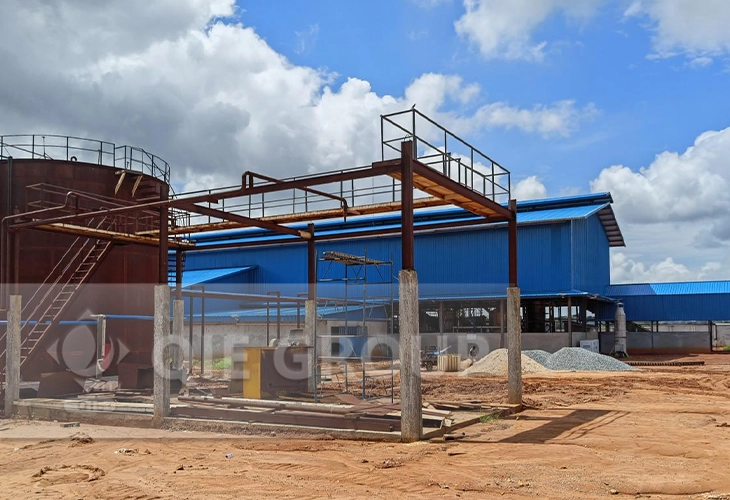


Our engineering team managed the full process from design to onsite commissioning, ensuring the system meets strict purity standards with low energy consumption.
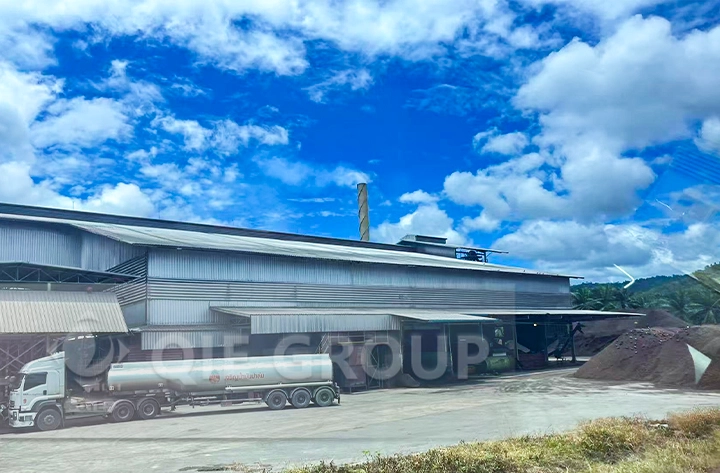
The plant maintains stable industrial operation and consistently meets international food-grade standards for output purity.